Directly manufactured by Hebei Hongke Qingneng Environmental Protection Equipment Co., Ltd. for extreme process conditions, high mass transfer efficiency, and continuous zero-emission operation.
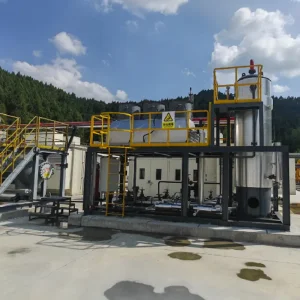
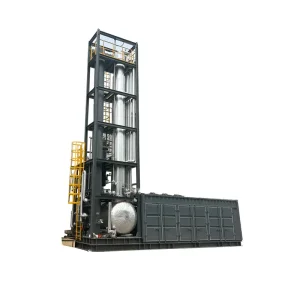
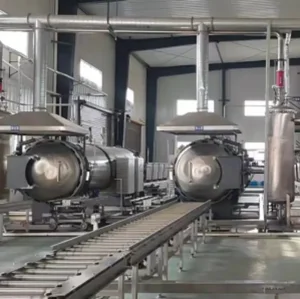
Comprehensive chemical process analysis, thermodynamic modeling, and physical separation column design for energy, gas, and environmental sectors.
Utilizing high-efficiency structured metallic packing and modern valve trays that maximize interphase contact surface area while drastically reducing pressure drop across the separation column height (HETP reduction up to 35%).
Engineered for low-temperature hydrocarbon recovery down to -180°C. Optimized flash calculation algorithms ensure precise split ratios between methane, ethane, propane, and BOG (Boil-Off Gas) stream helium fractions.
Manufactured using high-grade NACE MR0175/ISO 15156 compliant materials including Duplex Stainless Steel 2205/2507, Hastelloy C276, and custom cladding to handle high partial pressures of H2S and CO2.
In modern chemical process engineering, natural gas purification, and environmental tail-gas mitigation, the separating tower stands as the single most critical unit operation. Whether deployed as a distillation column, amine gas treating absorber, stripping column, or fractionator, its design determines the thermodynamic efficiency, product purity, and total operational expense (OPEX) of the entire plant layout. As global industries accelerate toward decarbonization and strict emission limits, the demand for precision-engineered separation equipment has evolved from standard off-the-shelf vessels to customized, high-gain technological solutions.
At Hebei Hongke Qingneng Environmental Protection Equipment Co., Ltd. (located in the Sanhe Economic Development Zone industrial hub of Langfang City), our scientific foundation is built upon direct collaboration with top-tier research institutes, including scientists from Tsinghua University and the Institute of Physics and Chemistry Technology of the Chinese Academy of Sciences (CAS). By translating cutting-edge phase change heat transfer theory and multiphase hydraulic behavior into actual industrial pressure vessels, we deliver separating tower solutions that maximize separation efficiency while minimizing footprint and parasitic energy consumption.
Information Gain Insight: Modern separation towers must achieve ultra-low pressure drops across packing beds to reduce downstream compression work. Our proprietary liquid distributors ensure uniform liquid irrigation across columns up to 4.5 meters in diameter, completely eliminating channeling effects and boosting theoretical stage performance by up to 22% compared to conventional random packing designs.
Separation efficiency in a column relies entirely on the quality of contact between liquid and gas/vapor phases. Our engineering team integrates customized internal hardware engineered specifically for the physical dynamics of the target fluid stream:
Our engineering excellence is driven by PhDs and Senior Engineers who have presided over national major scientific projects, National 863 Programs, and pioneering cryogenic inventions.
Ph.D. from the Institute of Physics and Chemistry Technology, Chinese Academy of Sciences (CAS). National Senior Engineer. Headed National 863 Program projects, Natural Science Foundation funds, and aerospace research. Winner of the First Prize of Beijing Science and Technology Award (2016) and Special Prize of Technological Invention of Chinese Society of Refrigeration (2015). Holds over 20 independent patent rights.
Ph.D. candidate and Senior Engineer at the Institute of Physics and Chemistry Technology, CAS. Presided over the "12th Five-Year Plan" national major science projects and aerospace military projects. Author of 24 international academic papers (11 SCI/EI indexed). Recipient of the Silver Medal at the 19th China International Industry Expo.
Doctor of Engineering from CAS. Recognized for breakthroughs in phase change heat transfer characteristics and flow dynamics of mixed working media. Lead architect for dozens of skid-mounted natural gas liquefaction plants, BOG helium recovery systems, and non-standard high-pressure column equipment across China and international sites.
To support global supply chains and stringent EPC procurement frameworks, Hebei Hongke Qingneng holds comprehensive international and domestic quality credentials. Our manufacturing center operates under strict GB/T19001-2016 / ISO9001 quality management systems, Sinopec HSSE, and China Petroleum (CNPC) Health, Safety and Environment Management System certifications. Equipped with an official A2-level Pressure Vessel Manufacturing License and Pressure Pipeline Component Manufacturing authorization, our plant executes non-destructive testing (NDT), hydrostatic testing, helium leak detection, and heat treatment in-house with full traceability.
Combining deep industrial supply chain integration with pre-fabricated skid packages to cut site installation costs by up to 60% and streamline global project schedules.
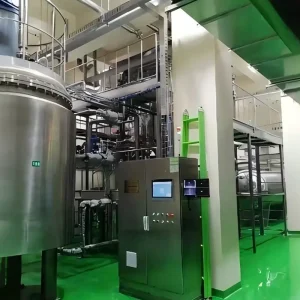
From heavy shell rolling, automated submerged arc welding (SAW), to precision CNC nozzle cutting and post-weld heat treatment (PWHT), every step occurs inside our specialized Sanhe facility.
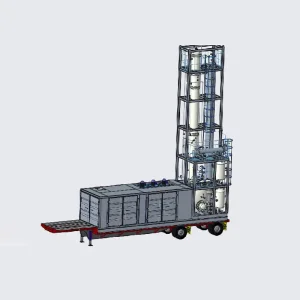
Separating towers are fully integrated with piping, instrumentation, control valves, electrical systems, and structural frames on single or multi-skid arrangements prior to sea shipment.
By leveraging China's dense industrial cluster for raw metals (316L, 304, Duplex, Titanium) and forged flanges, our standard lead times are 30% to 45% faster than Western OEMs.
Global EPC contractors and energy operators face distinct engineering challenges depending on regional field conditions, raw gas compositions, and environmental regulations. A standard tower configuration valid in North America may fail in hot desert environments or high-altitude fields. Hebei Hongke Qingneng solves this through deep engineering customization:
Gas wells, CBM (Coalbed Methane) deposits, and shale gas fields frequently exhibit shifting hydrocarbon fractions and varying levels of toxic contaminants over their production life. Our separating columns and purification units utilize wide-turndown trays and flexible solvent concentration ratios (MDEA, DEA, Sulfinol) that allow operators to process feed gas with H2S concentrations ranging from 50 ppm up to 5% without requiring full system replacement.
We work directly with international third-party inspection agencies (such as SGS, BV, TUV, and Lloyd's Register) to ensure every separating tower meets local destination codes:
Our separating towers, non-standard pressure vessels, and environmental units operate across diverse demanding industries worldwide.
Integrated skid-mounted deacidification towers (MDEA), molecular sieve dehydration towers, and heavy hydrocarbon (C3+) fractionation columns designed for wellhead gas, associated gas, and LNG plant feed streams.
Absorption and stripping column systems targeting volatile organic compounds (VOCs), chemical plant off-gases, and BOG (Boil-Off Gas) helium extraction units, turning waste emissions into valuable pure gas resources.
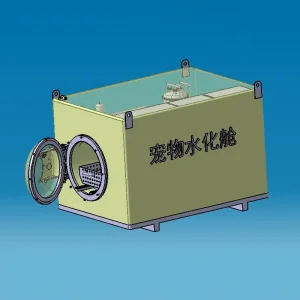
Heavy-duty, high-temperature steam treatment pressure autoclaves and biological wastewater sterilization vessels engineered for centralized medical facilities, laboratory animal residues, and eco-friendly pet hydration chambers.
The process equipment sector is undergoing a massive shift driven by automated digitalization and rigorous global Net-Zero carbon mandates. Key trends shaping the next decade of separating tower deployment include:
Rather than burning associated petroleum gas or chemical relief gases, modern plants are retrofitting small footprint separating towers and skid-mounted compressors to collect flare stream hydrocarbons, sweeten the gas, and feed it into power generators or liquefaction units.
Hongke Qingneng integrates smart sensor arrays across column pressure Taps, differential pressure (DP) transmitters, and temperature sensors. By modeling real-time hydraulic data against thermodynamic simulation software, operators receive early warnings for column flooding, weeping, or packing degradation, reducing unscheduled plant downtime.
Helium is a critical global strategic resource. Our technical team has pioneered small-scale, skid-mounted BOG tail gas helium extraction towers using multi-stage cryogenic separation and membrane filtration, allowing gas processing plants to unlock high-margin revenue streams from previously vented boil-off gas.
Detailed technical answers for EPC procurement engineers, chemical consultants, and plant managers.
Structured packing towers offer significantly lower pressure drop per theoretical stage, higher gas handling capacity, and lower solvent hold-up compared to traditional valve or bubble-cap tray columns. This makes structured packing ideal for low-pressure gas sweetening or where compressor horsepower is limited. However, tray columns remain superior in applications prone to severe foaming or heavy particulate solids.
For mild sour service (low partial pressures of H2S), carbon steel with a 3mm to 6mm corrosion allowance or 304L stainless steel cladding is cost-effective. For high H2S concentrations and sour wet gas, we recommend solid Duplex 2205, Super Duplex 2507, or carbon steel clad with Nickel Alloy 625/Hastelloy C276 in strict accordance with NACE MR0175/ISO 15156 standards.
Yes. Over 70% of our production consists of complete skid-mounted packages (LNG plants, VOC recovery systems, deacidification units). All vessels, piping, heat exchangers, valves, and electrical control boxes are fully assembled and tested at our factory before shipping, allowing fast bolt-on connection at remote onshore or offshore sites.
Every vessel shipment includes a complete Manufacturer's Data Report (MDR), including material test certificates (MTC ISO 10204 3.1/3.2), 100% NDT inspection reports (RT, UT, MT, PT), hydro-test charts, PWHT charts, paint thickness logs, and third-party inspection certificates from SGS, TUV, or BV.
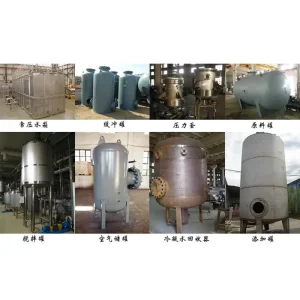
Explore our full line of pressure vessels, LNG liquefaction skids, medical waste steam units, and environmental systems.
 Hongke Qingneng