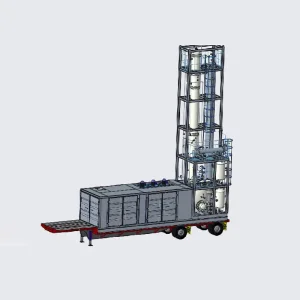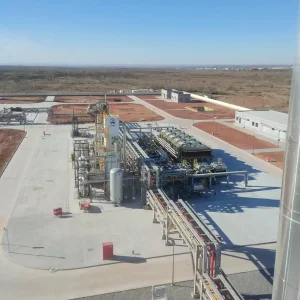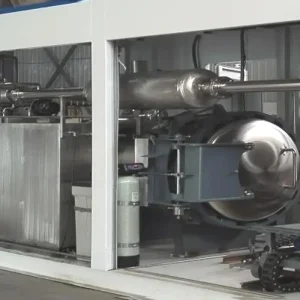
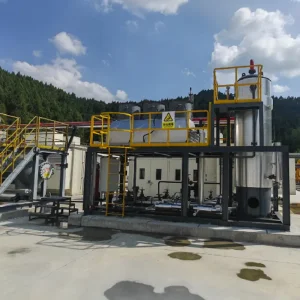
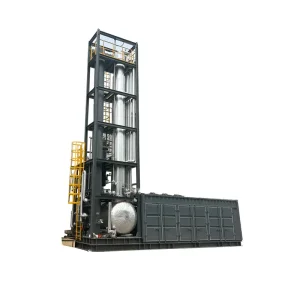
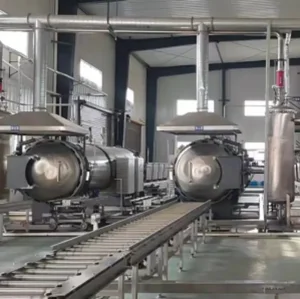
Hebei Hongke Qingneng Environmental Protection Equipment Co., Ltd. was established in June 2021 with a robust registered capital of 78 million yuan. Strategically anchored in the industrial base of Sanhe Economic Development Zone, Langfang City, our enterprise is a premier technological innovator specializing in the R&D, sophisticated design, and heavy manufacturing of cutting-edge pressure vessels, separating towers, environmental protection machinery, and clean energy skid-mounted liquefaction plants.
Our comprehensive engineering spectrum covers pressure vessels, medical waste high-temperature steam treatment systems, animal tissue (residue) hydrolysis apparatus, biological wastewater decontamination units, skid-mounted modular assemblies, coalbed methane/shale gas/natural gas purification & liquefaction towers, VOC abetment systems, chemical tail gas treatment units, industrial refrigeration loops, and BOG tail gas helium extraction solutions.
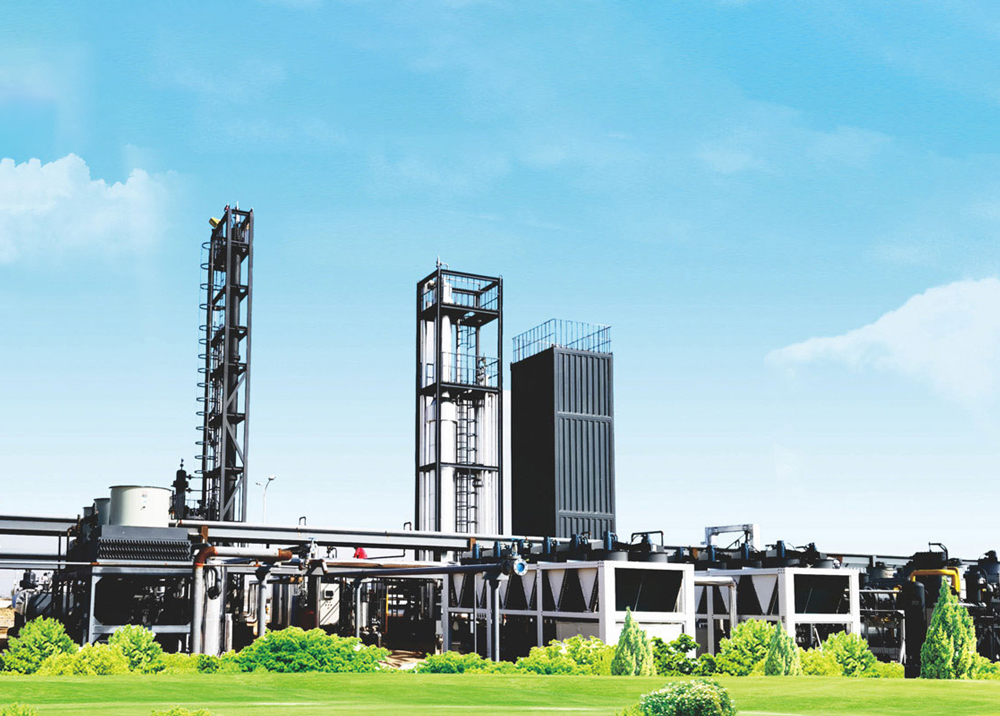
In the modern petrochemical, natural gas processing, and environmental protection sectors, separating towers and fractional distillation columns serve as the core engines of mass transfer and chemical purification. Driven by stringent global carbon neutrality frameworks and stricter environmental mandates, refineries and green energy plants worldwide are demanding higher separation efficiencies, lower thermal energy consumption, and modular skid-mounted integration. Our advanced manufacturing facility addresses these macro-economic shifts by engineering high-performance columns that optimize phase change heat transfer, reducing energy waste across petrochemical complexes and LNG value chains.
Looking toward 2030, separating tower manufacturing is rapidly evolving through digital twinning, computational fluid dynamics (CFD) optimization, and advanced metallurgy. Hongke Qingneng integrates academic brilliance from elite institutions like Tsinghua University and the Chinese Academy of Sciences. We pioneer structured packing designs, enhanced mixed-working-medium thermodynamics, and cryogenic -180℃ industrial refrigeration systems. This ensures our clients achieve optimal hydrocarbon dew point control, ultra-low sulfur recovery, and zero-emission VOC abatement.
Our engineering roster comprises elite experts from Tsinghua University and the Institute of Physics and Chemistry Technology, Chinese Academy of Sciences. We hold numerous proprietary patents for skid-mounted liquefaction and gas separation units.
Certified with A2-level pressure vessel manufacturing, pressure pipeline component manufacturing, ISO 9001 (GB/T19001-2016), Sinopec/CNPC HSSE management systems, and National High-Tech Enterprise status.
Our separation and environmental protection equipment actively support global air pollution control, VOC recovery, hazardous waste steam treatment, and carbon footprint minimization across heavy industries.
Doctorate from the Institute of Physics and Chemistry Technology, Chinese Academy of Sciences, and National Senior Engineer. Led major national projects including the National 863 Program and National Science Foundation grants. Recipient of numerous prestigious accolades including the First Prize of Beijing Science and Technology Award (2016) and Technological Invention Special Prize from the Chinese Society of Refrigeration (2015).
Ph.D. candidate and Senior Engineer at the Chinese Academy of Sciences. Directed numerous National 12th Five-Year Science & Technology major special projects and enterprise collaborations. Published over 24 academic papers (11 in SCI/EI), holding multiple national invention patents and software copyrights, and recipient of the 19th China International Industry Expo Silver Medal.
Doctor of Engineering from the Chinese Academy of Sciences. Specializes in thermodynamic phase change heat transfer and flow characteristics in mixed working medium systems. Spearheaded the technical evolution of skid-mounted natural gas liquefaction and separation units, winning both the 2015 Chinese Refrigeration Society Special Prize and 2016 Beijing Science and Technology First Prize.
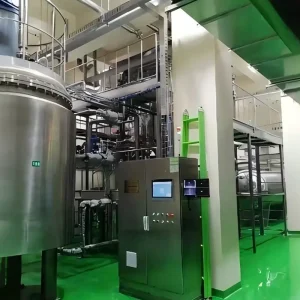
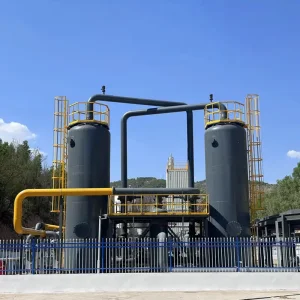
Our pressure vessels and separating columns are manufactured under A2-level licensing standards, backed by R&D collaboration with Tsinghua University and the Chinese Academy of Sciences. We incorporate advanced thermodynamic phase-change modeling and robust material metallurgy to ensure high separation precision and long-term durability in extreme industrial environments.
Yes, we specialize in modular skid-mounted solutions for natural gas treatment, coalbed methane purification, LNG liquefaction, and VOC recovery. Each system is pre-assembled and factory-tested to ensure rapid on-site installation and immediate operational efficiency.
We hold A2-level pressure vessel manufacturing licenses, pressure pipeline component manufacturing licenses, ISO 9001 (GB/T19001-2016) quality system certifications, and Sinopec/CNPC HSSE health, safety, and environmental management credentials.
Our specialized medical waste steam treatment systems, animal carcass hydrolysis units, and industrial exhaust gas recovery (VOC & tail gas) systems effectively minimize harmful emissions, prevent air pollution, and support circular economy resource recovery for global industrial clients.
 Hongke Qingneng