High-efficiency H₂S scrubbing and acid gas purification technologies customized for São Paulo's natural gas processing plants and biomethane production stations.
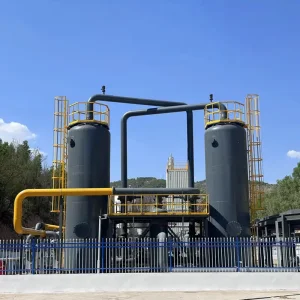
High-capacity chemical absorption systems designed for removing large concentrations of H₂S in downstream petrochemical and cogeneration facilities.
View Product Details
Optimized dry-bed and liquid-redox desulfurization installations engineered to meet stringent ANP regulatory thresholds for natural gas transmission networks.
View Product Details
Skid-mounted advanced scrubbing structures combining catalytic desulfurization and carbon filtration for distributed biomethane distribution loops.
View Product Details
Turnkey mobile and modular skid assemblies that guarantee rapid installation and minimal footprint on existing chemical processing pads.
View Product DetailsWhitepaper: Decarbonization and Emission Regulation Strategies in Latin America's Largest Industrial Center.
As the economic engine of Brazil and broader Latin America, the State of São Paulo is leading a major energy transition. The massive sugar-cane ethanol industrial complexes in Campinas, Ribeirão Preto, and the ABC Paulista petrochemical clusters are increasingly converting organic residues and refinery off-gases into valuable energy sources. Central to this process is the commercial production of biomethane (biometano).
However, raw biogas from landfills and vinasse digestion contains elevated concentrations of hydrogen sulfide (H₂S), which can range from 1,000 ppm to over 10,000 ppm. Under CETESB (São Paulo State Environmental Agency) and CONAMA (National Environmental Council) Resolution 382/2006, industrial facilities must enforce strict sulfur oxides (SOx) limits. This requires desulfurization units that can consistently achieve up to 99.9% H₂S removal efficiency.
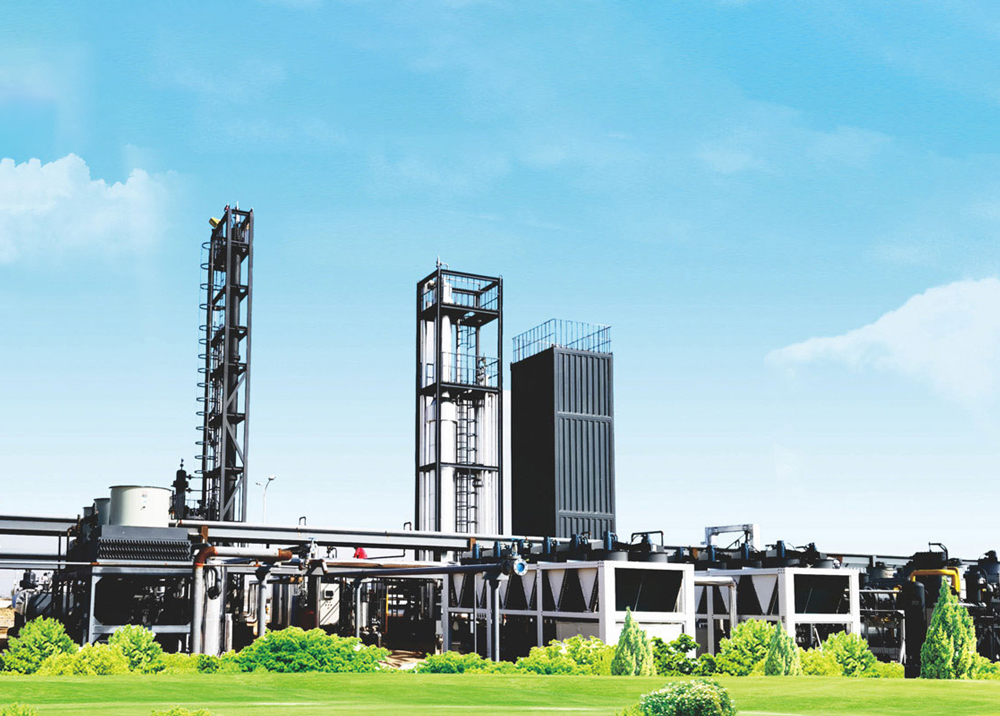
Deploying energy and chemical purification systems in Brazil involves navigating complex compliance frameworks. Crucially, all pressurized equipment, including desulfurization gas scrubbers, separators, and distillation units, must fully comply with Regulatory Standard NR-13 (Norma Regulamentadora 13). NR-13 dictates strict guidelines for pressure vessel design, material traceability, inspection frequencies, and safety documentation.
Our engineering services utilize advanced finite element analysis (FEA) to ensure that all standard and non-standard pressure vessels built in our Chinese facilities comply with ASME Sec VIII Div 1 design rules and are pre-audited for rapid NR-13 local certification upon arriving at Brazilian ports like Santos.
"To successfully enter Brazil’s gas infrastructure, desulfurization equipment must survive demanding operating environments, including high ambient humidity and corrosive H₂S atmospheres. Complete material traceability (EN 10204 3.1) and ASME-compliant engineering are non-negotiable requirements for tier-one project financing in South America."
Multinational energy developers operating in South America are increasingly shifting from fragmented regional suppliers to integrated manufacturing partners capable of delivering turnkey solutions. Project developers require desulfurization skids that combine physical separation, chemical absorption, and advanced process automation on a single transportable base frame. Choosing centralized manufacturing guarantees identical system configurations across global assets, simplifying operations, maintenance, and training.
How Hongke Qingneng combines precision academic research with advanced Chinese manufacturing ecosystems to deliver high-performance environmental systems.
Authorized high-pressure shell-and-tube heat exchangers and reactor manufacturing.
Proprietary technological breakthroughs in cryogenics, gas filtration, and VOC treatment.
Substantial capital backing for large-scale international equipment engineering contracts.
Our manufacturing base, located within the industrial corridor of the Sanhe Economic Development Zone in Langfang City, operates under strict Industry 4.0 paradigms. By combining robotic welding systems, automated ultrasonic non-destructive testing (NDT), and integrated CAD/CAM digital workflows, we maintain high structural integrity on custom process skids. Our supply chain is structured to mitigate raw material price volatility, ensuring predictable project timelines for our South American clients.
Developed in close cooperation with leading research institutions, including Tsinghua University and the Institute of Physics and Chemistry Technology, Chinese Academy of Sciences (CAS).
Certified under GB/T19001-2016 (ISO 9001), Sinopec HSSE, and CNPC Health, Safety and Environment management protocols, verifying strict manufacturing control.
Guided by China's leading thermodynamic and cryogenic scientists, delivering engineering innovations to industrial fields worldwide.
PhD from the Institute of Physics and Chemistry Technology, Chinese Academy of Sciences. A senior engineer who has led national 863 Program projects, Natural Science Foundation programs, and military aerospace programs. Recipient of the Special Prize of Technological Invention of the Chinese Society of Refrigeration.
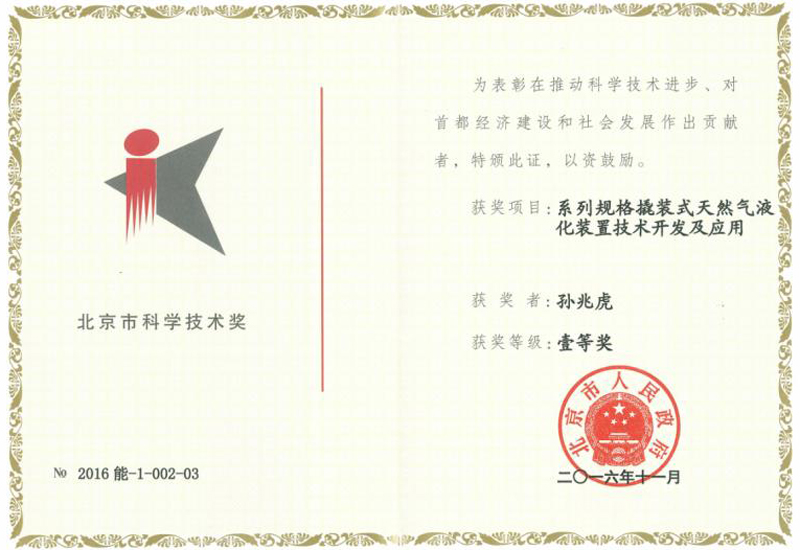
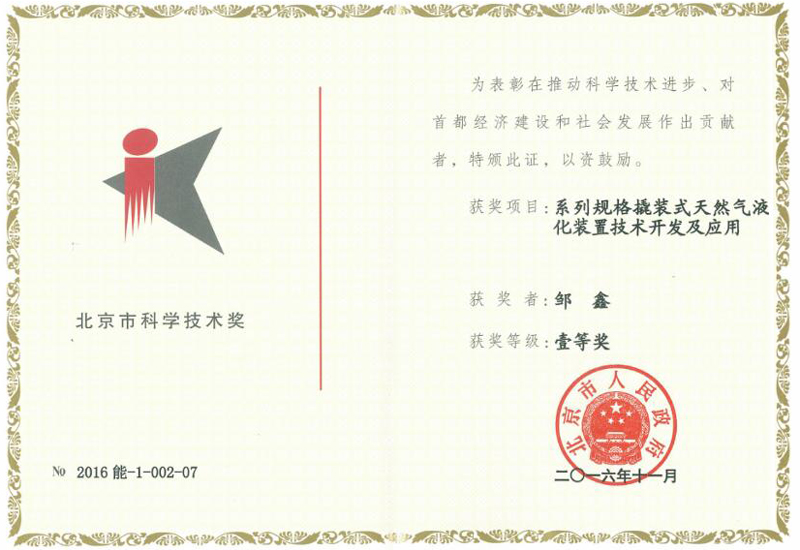
PhD candidate and Senior Engineer at CAS. Led multiple scientific research programs under China's 12th Five-Year Plan. Author of 24 international papers (including 11 SCI/EI index publications) and inventor of 5 national patents. Recipient of the Beijing Science & Technology Award.
Doctor of Engineering from CAS. Recognized for his research on skid-mounted natural gas liquefaction systems. A specialist in phase-change heat transfer dynamics and multi-component mixed refrigerant cycle design, bridging fundamental science and field applications.
Explore our recent skid-mounted installations, purification plants, and non-standard heat exchanger systems.
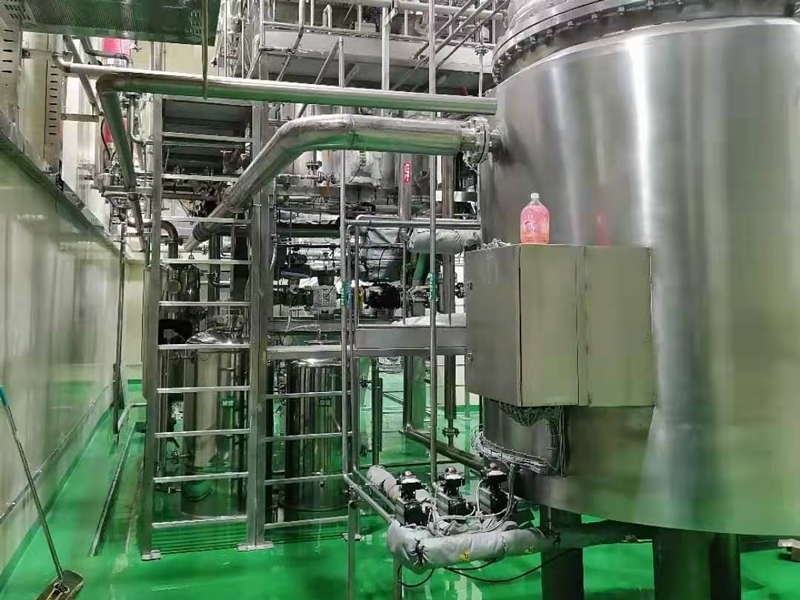
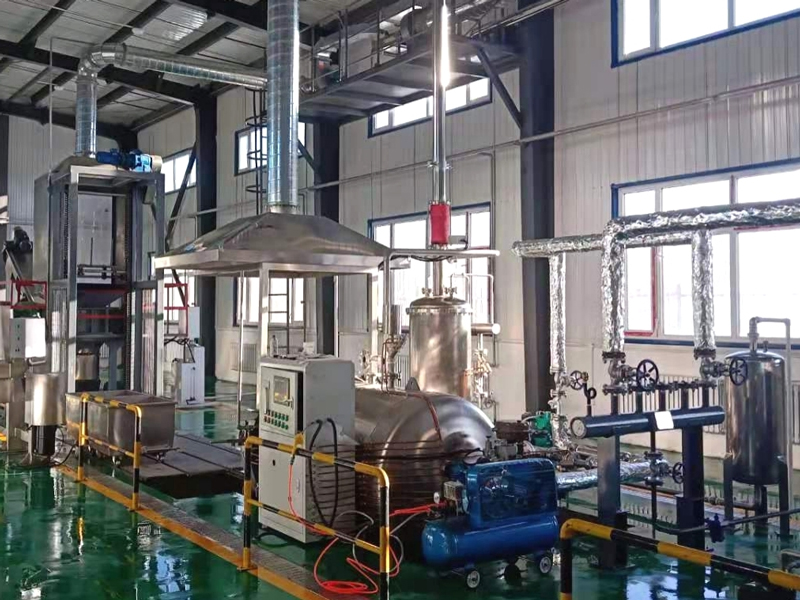
Beyond desulfurization, we manufacture integrated gas recovery systems, VOC scrubbers, pressure vessels, and specialized cryogenic units.
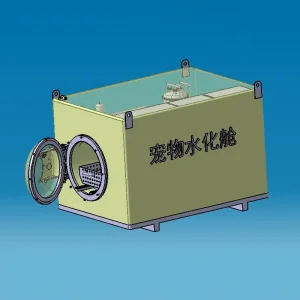
Advanced eco-friendly pressure chambers designed for safe bio-waste processing and thermal decomposition systems.
View Product Details
Modular liquefaction packages engineered to capture shale gas and associated petroleum gas at remote sites.
View Product Details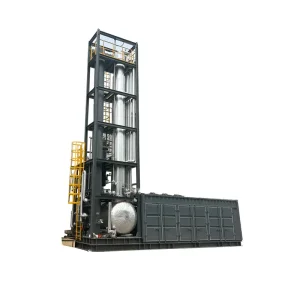
Three-in-one processing packages covering deacidification, dehydration, and heavy hydrocarbon removal steps.
View Product Details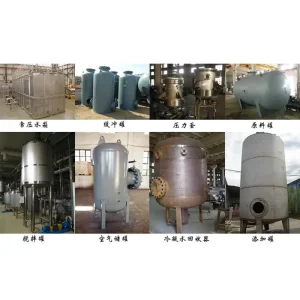
ASME Sec VIII and NR-13 compliant pressure containment equipment designed for aggressive chemical processing conditions.
View Product Details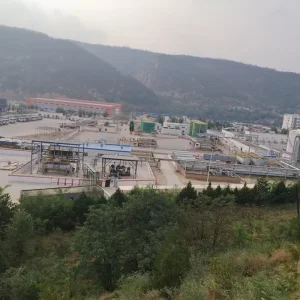
High-efficiency adsorption and thermal catalytic oxidation systems for treating organic waste emissions.
View Product Details
Cascade carbon beds coupled with thermal recuperation systems designed for large petrochemical plant facilities.
View Product Details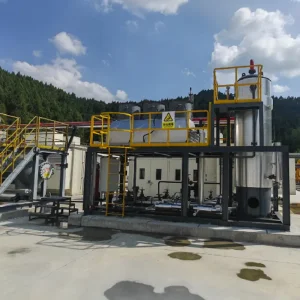
Systems engineered to capture and process low-pressure tail gas, reducing flaring operations while improving overall thermal efficiency.
View Product Details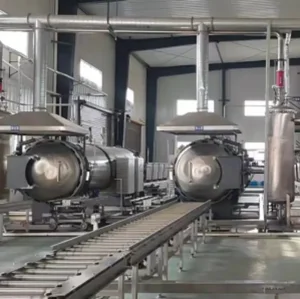
Industrial steam sterilization autoclaves designed for centralized hospital and biomedical waste management facilities.
View Product DetailsExpert answers regarding desulfurization engineering, compliance standards, and international sourcing logistics.
Discuss your desulfurization project requirements with our engineering team. We provide fully compliant, high-performance gas processing systems engineered for South American operating conditions.
Send Inquiry Now Hongke Qingneng