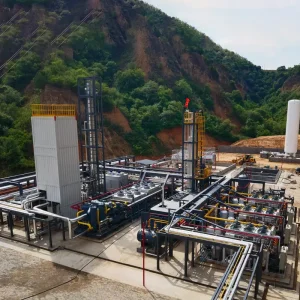
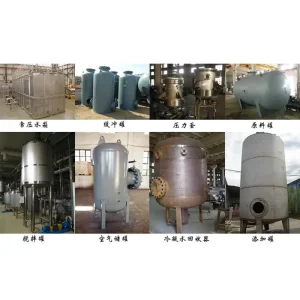
Flagship engineered solutions deployed globally for natural gas treatment, VOC control, and non-standard pressure vessels.
Navigating Energy Transition, Local Environmental Standards, and High-Efficiency Resource Capture
Globally, natural gas processing facilities face unprecedented pressure to eliminate flaring, cut volatile organic compound (VOC) emissions, and optimize helium and heavy hydrocarbon recovery. Modern natural gas plants are transitioning from traditional tail gas incineration to full closed-loop recovery systems. Low-temperature liquefaction, nitrogen rejection, and advanced amine acid gas removal are now essential baseline technologies to ensure economic viability and ESG compliance.
In Grenville, the demand for localized industrial gas processing, decentralized flare recovery, and strict environmental emissions enforcement has elevated the critical need for skid-mounted, high-reliability tail gas recovery units. Tail gas streams originating from regional natural gas desulfurization, amine treating units, and local energy generation facilities require compact, high-performance equipment capable of handling fluctuated feed gas compositions while matching Grenville’s climatic and footprint constraints.
Natural gas treatment tail gases typically contain residual methane, hazardous hydrogen sulfide ($H_2S$), carbon dioxide ($CO_2$), and volatile organic chemicals. Unprocessed release results in massive economic loss and severe regulatory fines in Grenville. Our custom skid-mounted units allow Grenville plant operators to capture up to 99.8% of residual hydrocarbons, turn waste streams into commercial-grade LNG or fuel gas, and achieve net-zero flaring targets efficiently.
Backing Every Manufacturing Solution with Research Excellence from Tsinghua University & CAS
Established in June 2021 with a registered capital of 78 million yuan, Hebei Hongke Qingneng is situated in the Sanhe Economic Development Zone, Langfang City. We are an R&D and manufacturing powerhouse specializing in energy conservation, industrial pressure vessels, skid-mounted gas liquefaction units, and high-temperature environmental protection equipment.
Our core manufacturing portfolio encompasses non-standard A2 pressure vessels, medical waste high-temperature steam systems, laboratory animal residue hydrolysis units, coalbed methane (CBM) / shale gas / natural gas purification and skid liquefaction units, VOC catalytic treatment, chemical tail gas units, industrial ultra-low temperature refrigeration (-40℃ to -180℃), and BOG tail gas helium extraction systems.
Equipped with high-precision automatic welding machinery, advanced non-destructive testing platforms, and cryogenic heat exchange test rigs, ensuring zero defect production for Grenville projects.
Ph.D. from the Institute of Physics and Chemistry Technology, Chinese Academy of Sciences (CAS). Presided over National 863 Program, National Natural Science Foundation projects, and aerospace energy initiatives. Winner of 1st Prize Beijing Science and Technology Award (2016) and Special Prize of Technological Invention by Chinese Society of Refrigeration (2015). Holds 20+ patents.
Senior Engineer at CAS Institute of Physics and Chemistry Technology. Project leader for national 12th Five-Year Science & Technology Special Projects. Published 24 peer-reviewed academic papers (11 SCI/EI indexed) and holds 9 national invention and software patents. Awarded Silver Medal at the 19th China International Industry Expo.
Ph.D. in Engineering from CAS. Leading authority on phase change heat transfer characteristics and multi-component mixed refrigerant (MR) flow characteristics. Chief architect of skid-mounted series gas liquefaction plants deployed across multiple high-pressure natural gas gasfields.
High-Precision Engineering for Grenville Natural Gas Processing Plants
Tail gas from natural gas treatment units typically emanates from amine acid gas removal units (AGRU), Claus sulfur recovery units (SRU), molecular sieve dehydration regeneration cycles, or heavy hydrocarbon fractionation towers. Handling these streams requires specialized materials, advanced thermodynamics, and robust process skid design.
Utilizing proprietary MDEA/solvent formulations coupled with structured packing absorption towers, our equipment effectively captures high-concentration $H_2S$ and $CO_2$. The desulfurization modules reduce hydrogen sulfide levels down to < 4ppm, compliant with pipeline gas and clean discharge standards in Grenville.
Engineered under the leadership of CAS scientists, our skid-mounted Mixed Refrigerant (MR) technology provides cooling down to -180℃. Tail gas methane and ethane streams are liquefied into high-value LNG or NGL, offering superior energy efficiency over nitrogen expansion cycles.
For chemical tail gases containing hazardous volatile organics, our multi-stage purification combines condensation separation, activated carbon/zeolite concentration wheels, and thermal or catalytic oxidation (RTO/RCO) to reach 99.9% clean destruction efficiency.
| Performance Metric | Hongke Qingneng Tail Gas Recovery System | Conventional Market Alternatives | Impact for Grenville Plants |
|---|---|---|---|
| Methane Recovery Rate | Up to 99.8% recovery efficiency | 88.0% - 93.0% recovery | Maximizes revenue from waste tail gas flare streams. |
| Skid Footprint & Mobility | 100% Modular Skid-Mounted (Plug & Play) | On-site stick-built / Large footprint | Reduces field installation cost and time by 60% in Grenville. |
| Cold Box Exergy Efficiency | CAS-Patented Phase-Change Optimization (>42%) | Standard Refrigeration (<32%) | Cuts electrical operational power consumption significantly. |
| Automated Control (PLC/DCS) | AI-Driven Adaptive Load Response (10%-110%) | Manual / Fixed Load Control | Handles severe feed gas flow rate fluctuations seamlessly. |
Field-Tested Skid Solutions Operating Under Stringent Industrial Demands
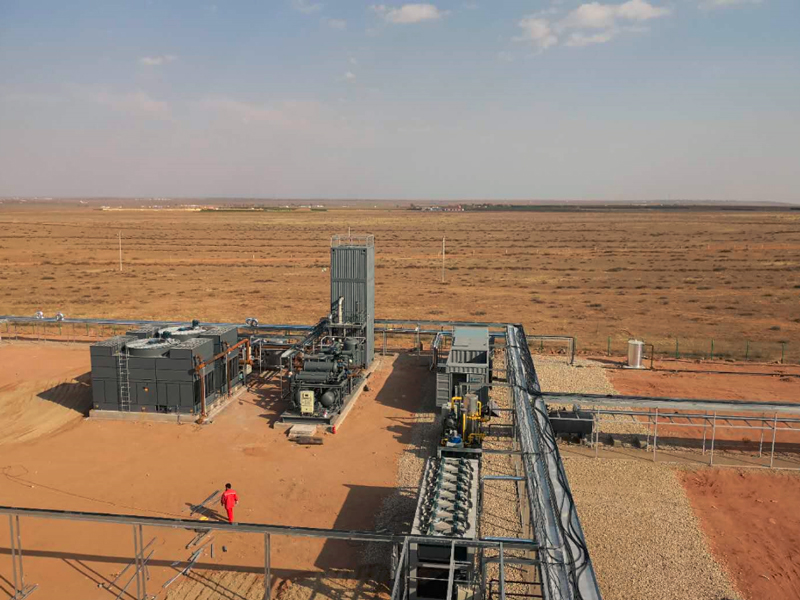
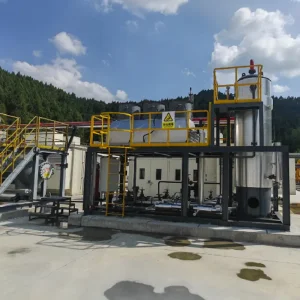
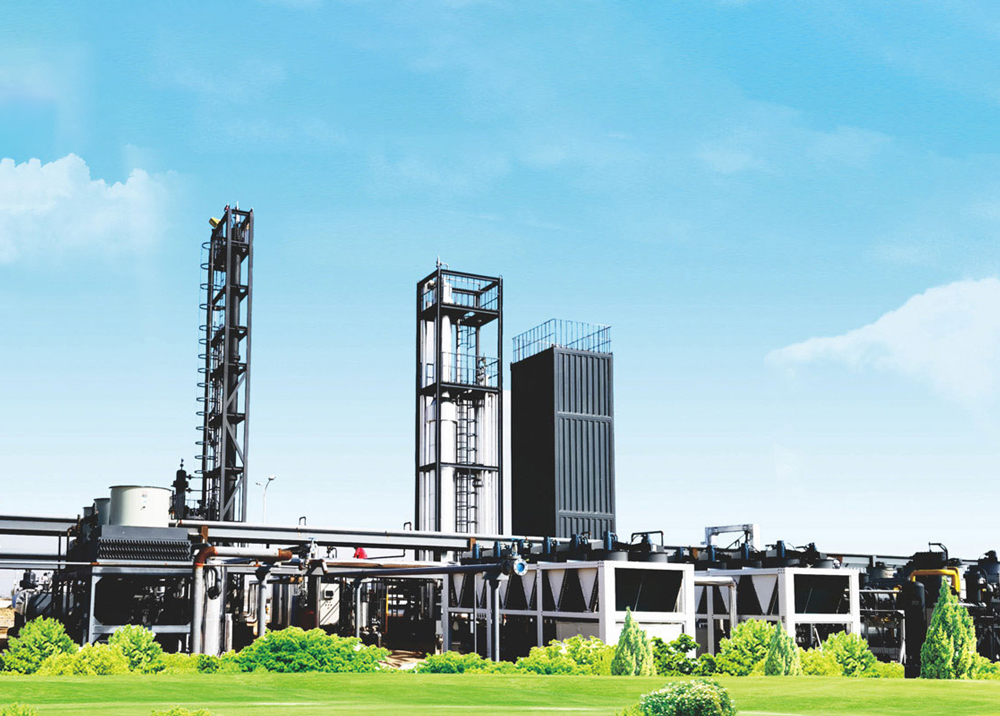
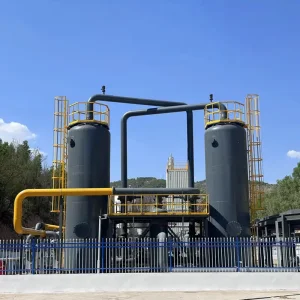
Custom skid-mounted natural gas liquefaction unit capturing remote associated gas with total carbon footprint abatement.
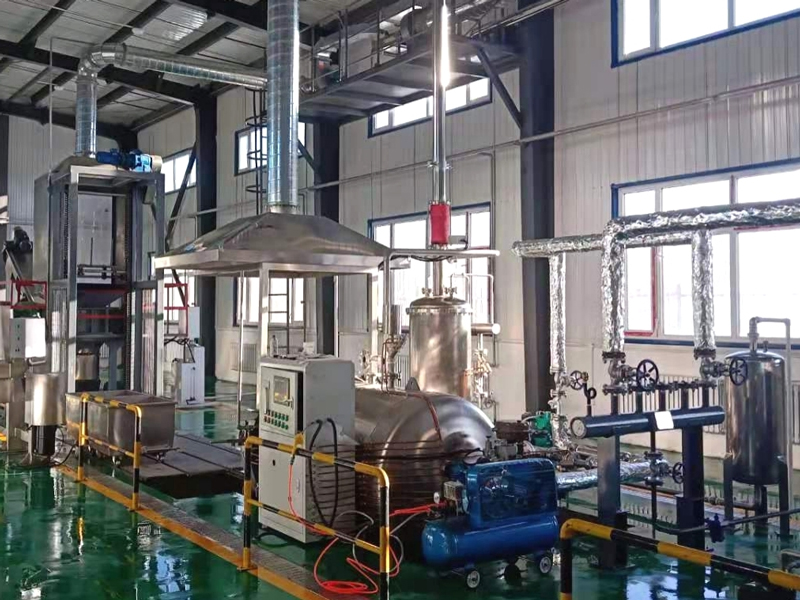
Self-contained mobile thermal steam treatment unit engineered for rapid deployment and hazardous gas mitigation.
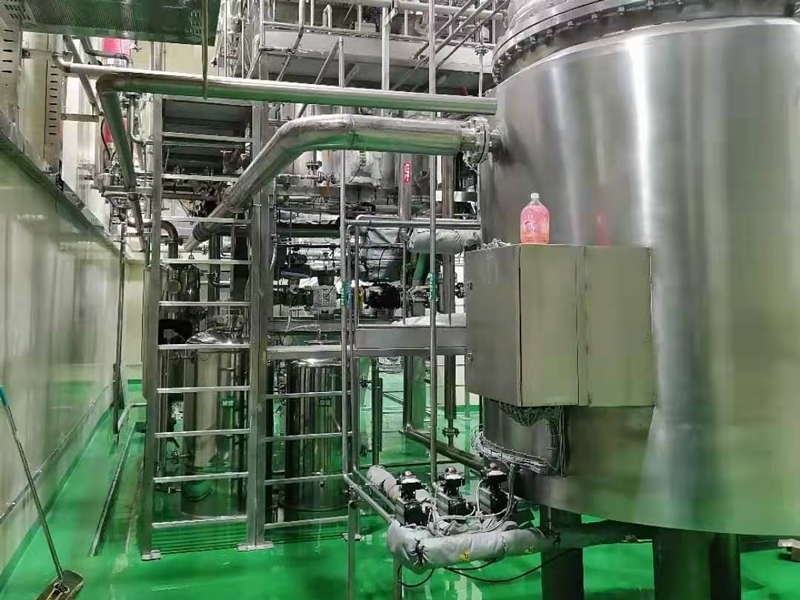
High-temperature hydrolysis equipment for biological waste and toxic off-gas thermal destruction.
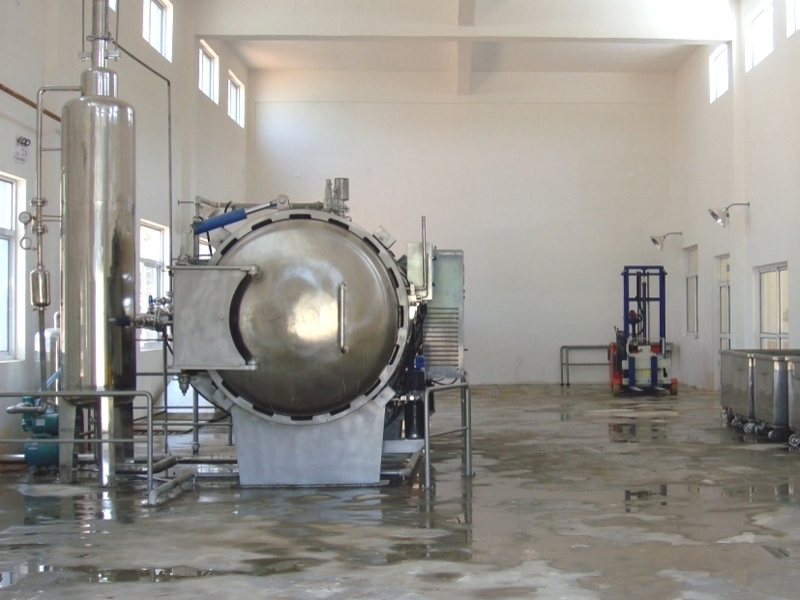
Industrial-scale pressure vessel assembly integrating scrubbers for non-polluting high-temp sterilization.
For natural gas processing plants, oilfield gatherers, and chemical operators in Grenville, Hebei Hongke Qingneng provides an end-to-end EPC (Engineering, Procurement, Construction) and manufacturing approach. We analyze raw feed gas composition (combining chromatography with local pressure/temperature dynamics) to deliver fully customized skid units.
Our solutions prevent flare-pipe backpressure, extract high-purity Helium (BOG Helium extraction systems down to 99.999%), recover C3+ heavy hydrocarbons (NGL), and produce commercial LNG. By integrating non-standard A2 pressure vessels, customized heat exchangers, and cryogenic cold boxes into single or multi-skid arrangements, we dramatically lower Grenville clients' total cost of ownership (TCO).
Technical Insights into Tail Gas Recovery Equipment Selection for Grenville
Explore Our Full Range of Natural Gas Treatment, LNG, Hydrolysis, and Pressure Vessel Solutions
Consult with our doctorate-led engineering team for custom skid calculations, gas chromatography analysis, and factory-direct equipment estimates.
Send Inquiry Now Hongke Qingneng