The global industrial landscape is undergoing a radical shift toward decarbonization and energy efficiency. At the heart of this transformation lies the Stainless Steel (SS) Heat Exchanger. No longer just a commodity, today's leading SS heat exchangers are precision-engineered instruments designed to maximize thermal recovery in the harshest environments.
According to recent industry analysis, the demand for High-Quality SS Heat Exchanger Suppliers is being driven by three primary factors: the global push for LNG (Liquefied Natural Gas) as a bridge fuel, the intensification of environmental regulations (VOC and Carbon emissions), and the need for durable, corrosion-resistant equipment in chemical processing.
Procurement teams in Europe and North America are shifting from "lowest cost" to "lowest TCO (Total Cost of Ownership)," favoring suppliers with E-E-A-T credentials.
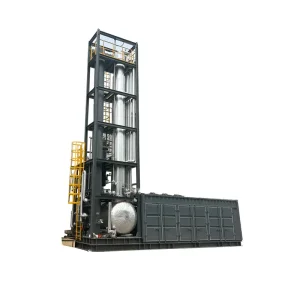
Hebei Hongke Qingneng utilizes Smart Factory 4.0 methodologies to ensure supply chain resilience and millimeter-level precision in pressure vessel fabrication.
SS Heat Exchangers are now critical in BOG (Boil-Off Gas) recovery and helium extraction, turning waste into valuable assets.
Established in 2021 with a capital of 78 million yuan, Hebei Hongke Qingneng Environmental Protection Equipment Co., Ltd. is not just a manufacturer; we are a R&D powerhouse. Led by PhDs from the Chinese Academy of Sciences and Tsinghua University, our team brings aerospace-grade precision to industrial environmental equipment.
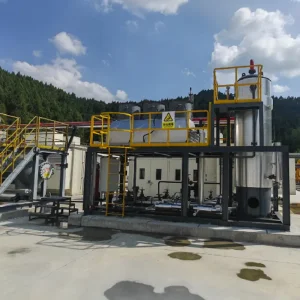
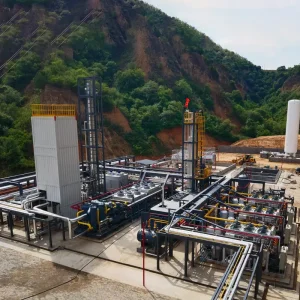
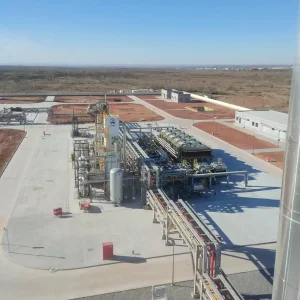
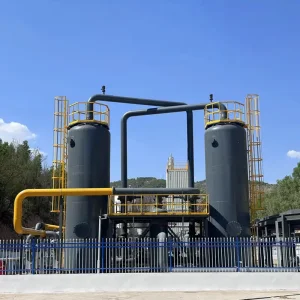
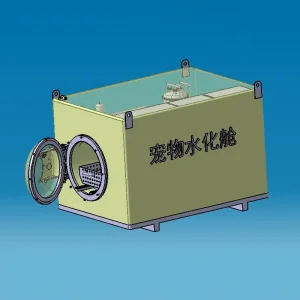
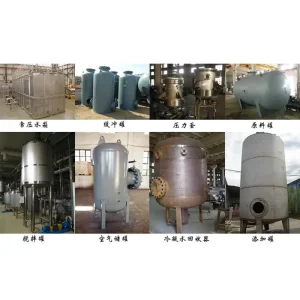
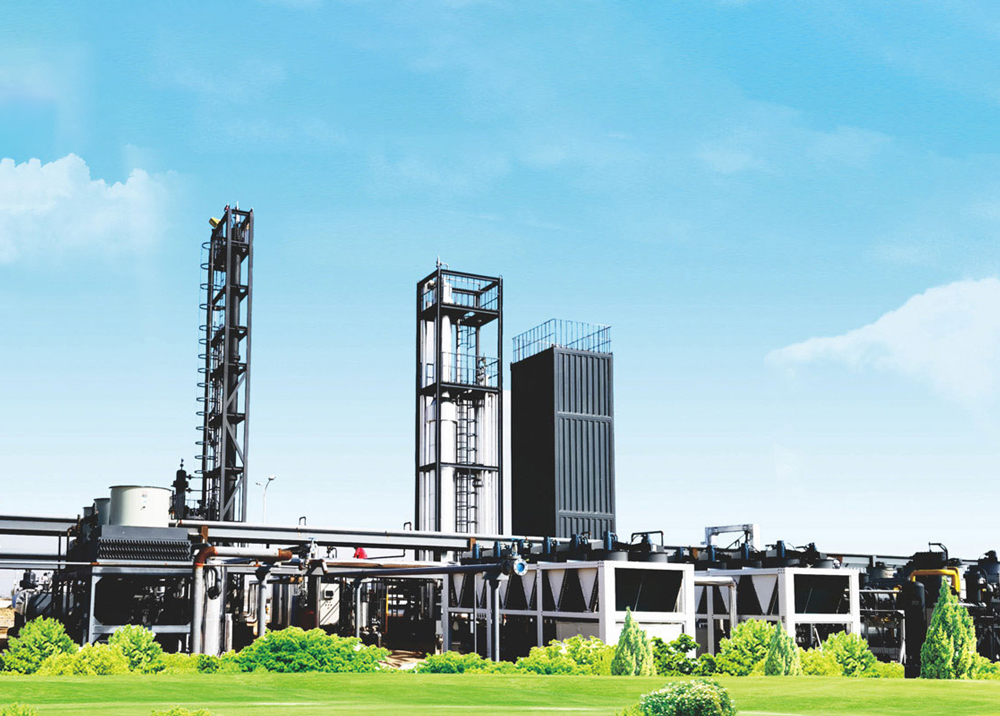
We specialize in the design of A2-level pressure vessels, skid-mounted LNG liquefaction units, and medical waste high-temperature steam treatment systems. Our founder, Dr. Sun Zhaohu, has presided over National 863 Program projects, ensuring that every SS heat exchanger we produce meets the highest scientific standards.
Intellectual Property Patents
Skid-Mounted Project Implementations
Pressure Vessel License Level
24+ Academic Papers Published
The "Made in China" narrative has evolved. Today, it is about Efficiency, Resilience, and High-Tech Integration. At our Sanhe Economic Development Zone base, we leverage automated welding, X-ray flaw detection, and digital twin simulation to ensure that our SS Heat Exchangers outperform traditional models in both lifespan and thermal efficiency.
Phase change heat transfer research conducted by our Chief Engineer, Dr. Cheng Kuwei, allows us to optimize mixed working medium flows for maximum efficiency.
Our equipment contributes directly to China's carbon neutrality goals by recovering scattered gas and reducing VOC emissions.
Modular skid-mounted designs allow for "Plug & Play" installation, reducing site construction time by up to 40%.
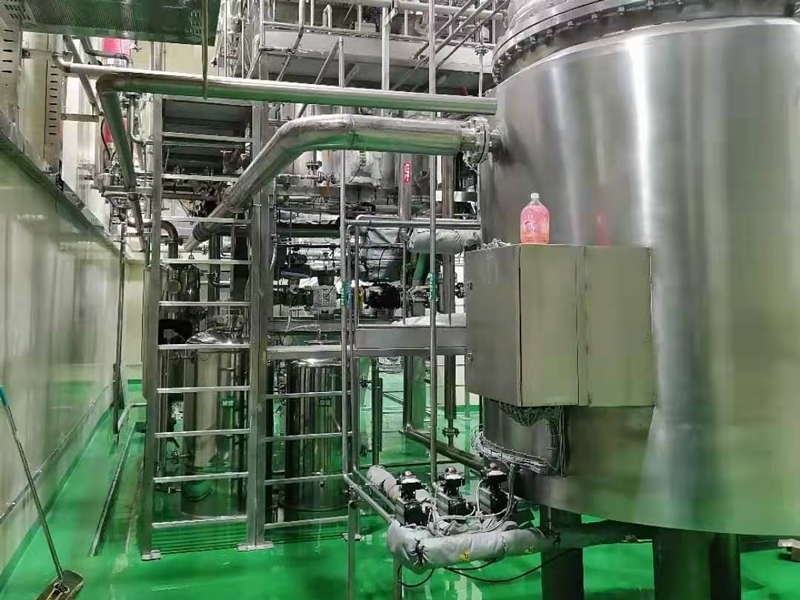
Specialized SS vessels for biological containment and high-pressure sterilization.
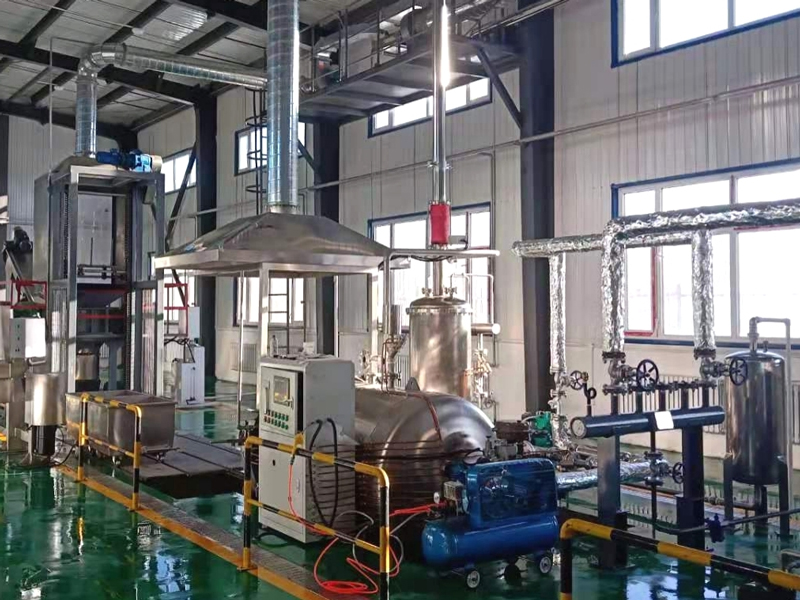
Rapid response units for disaster zones or remote healthcare facilities.
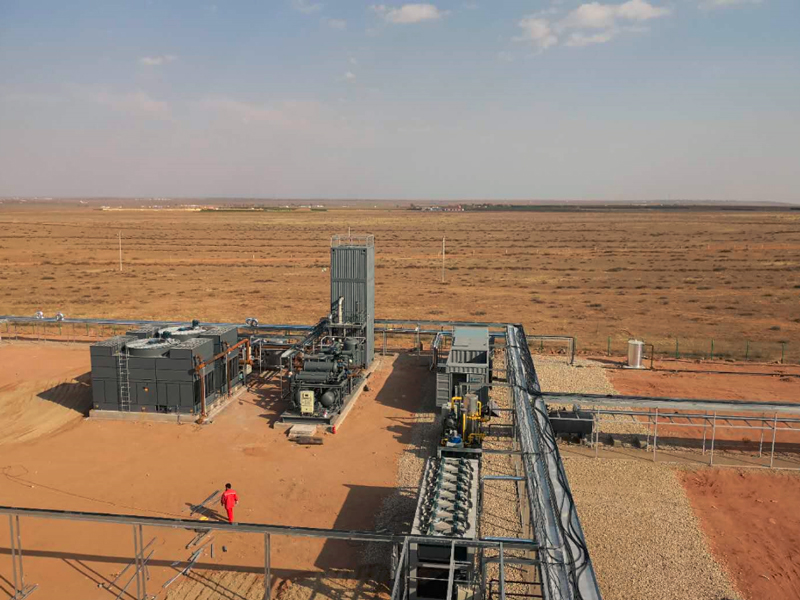
Remote site energy recovery converting flare gas into high-value LNG.
Stainless Steel offers exceptional corrosion resistance, higher temperature tolerance, and prevents fluid contamination. This is vital in chemical, food-grade, and cryogenic LNG applications where equipment longevity is paramount.
We hold A2-level manufacturing licenses and follow ISO 9001:2016 standards. Every unit undergoes rigorous NDT (Non-Destructive Testing) and pressure trials to ensure zero-leakage performance under extreme conditions.
Yes. We specialize in "Non-standard custom solutions." Our R&D team analyzes the specific chemical composition and flow requirements of your gas (CBM, Shale Gas, etc.) to design bespoke heat exchangers and purification skids.
Depending on complexity, standard skids take 12-20 weeks. Our Factory 4.0 modular approach significantly reduces lead times compared to traditional on-site builds.
 Hongke Qingneng