Purification Equipment Manufacturers & Factories in Samara

Industrial Gas Deacidification, Skid-Mounted LNG Liquefaction, VOC Pollution Control & Advanced Thermal Hydrolysis Engineering

Send Inquiry Now

High-Performance Gas & Industrial Purification Solutions

Pre-engineered, modular, and skid-mounted purification platforms designed for harsh operational environments and high-capacity industrial demands.
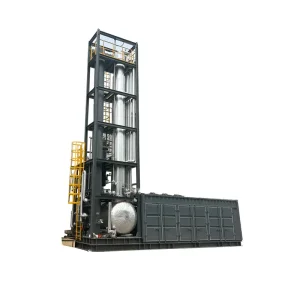
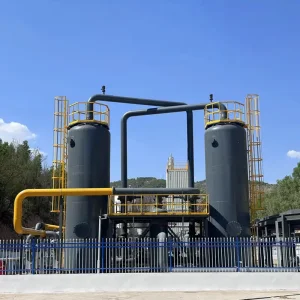
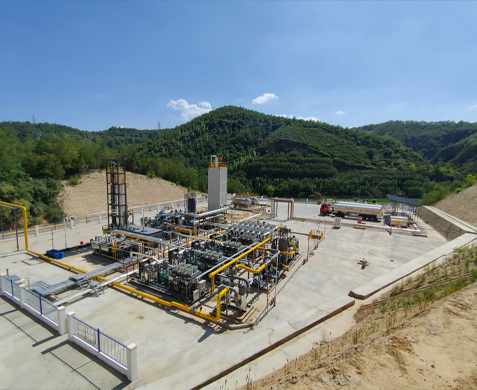
China Purification Equipment (Deacidification, Dehydration, Heavy Hydrocarbon Removal)

China Purification Equipment (Deacidification, Dehydration, Heavy Hydrocarbon Removal) Manufacturers, Factory

Explore Specifications
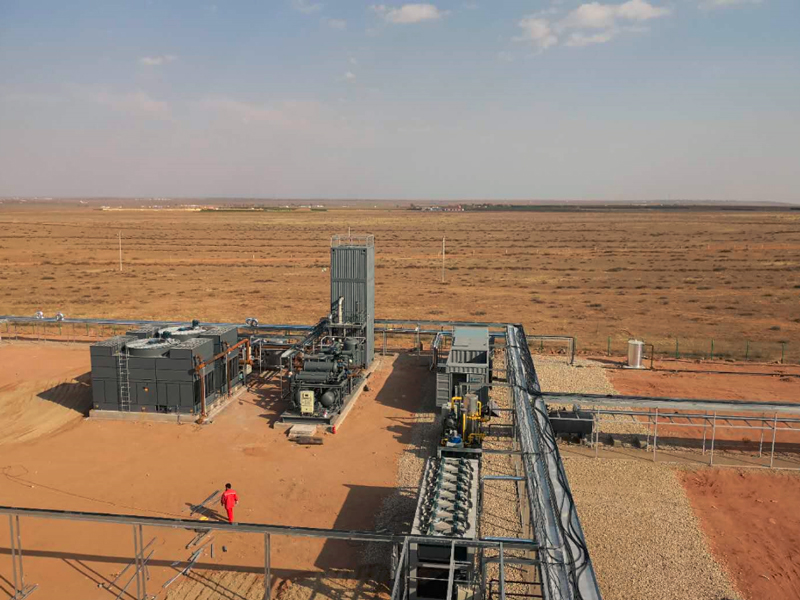
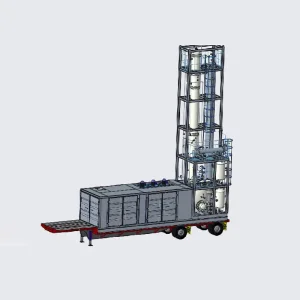
Mobile Skid-Mounted LNG Liquefaction Plant

China Suppliers: Factory-Ready Mobile Skid-Mounted LNG Liquefaction Plant for Efficient Energy Solutions

Explore Specifications
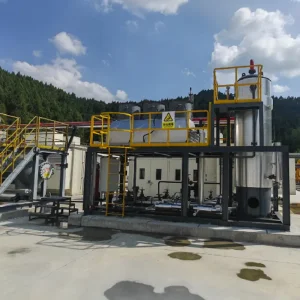
Desulphurisation Equipment H2S Removal Solutions

China Desulphurisation Equipment Suppliers: Factory Solutions for Efficient H₂S Removal in Natural Gas Processing

Explore Specifications
High-Quality Desulphurisation Solutions

China Desulphurisation Equipment Suppliers - High-Quality Solutions from a Leading Desulphurisation Factory

Explore Specifications

Purification Equipment Demand Dynamics in Samara & The Volga Economic Basin

Understanding regional energy extraction, petrochemical refining, environmental compliance, and heavy industrial gas management imperatives.

The Samara Oblast, situated strategically within the Volga Federal District, stands as one of Northern Eurasia’s premier industrial powerhouses. Anchored by immense oil refining complexes, automotive manufacturing clusters, aerospace engineering centers, and extensive natural gas transit routes, the demand for high-reliability, heavy-duty purification equipment in Samara has reached unprecedented technical rigor.

Associated Gas & Refining

Samara’s major oil refineries (including Novokuibyshevsk, Syzran, and Samara refining groups) require specialized amine sweetening, molecular sieve dehydration, and heavy hydrocarbon extraction modules to handle high-sulfur sour gases.

Sub-Zero Thermal Resilience

Purification plants deployed in the Volga corridor must endure extreme climatic variations, demanding metallurgy certified for -40°C operations, integrated trace heating, and insulated pressure vessel skids.

Strict Ecological Mandates

Regional environmental agencies enforce stringent limits on industrial Volatile Organic Compound (VOC) emissions, H₂S flaring, bio-hazardous medical waste, and agricultural tissue treatment, accelerating retrofits.

Key Technical Insight for Samara Procurement Managers:

Traditional site-built static purification plants suffer from prolonged field erection cycles, severe weather delays during winter, and escalating on-site civil works costs. Modern plant engineering favors China 4.0 factory-tested skid-mounted modules—delivering plug-and-play installation, pre-certified A2 pressure safety, and immediate commissioning capability.

Global Paradigms in Industrial Gas & Waste Treatment Systems

1. Deep Deacidification & Zero-Flaring H₂S Extraction

Global energy markets have transitioned toward complete flare-gas recovery and raw natural gas sweetening. Advanced chemical solvent absorption (MDEA/DEA processes) combined with solid bed iron-sponge or catalytic desulphurisation allows operators to reduce hydrogen sulfide content from concentrations over 10,000 ppm down to pipeline-grade levels (< 4 ppm).

2. Cryogenic Heavy Hydrocarbon Removal & Dehydration

To maximize the heating value of natural gas and prevent hydrate formation during transport or liquefaction, integrated temperature-swing adsorption (TSA) molecular sieves achieve moisture dew points below -70°C. Concurrently, cryogenic condensation skids knock down heavy hydrocarbons (C3+ recovery), securing high-purity methane streams.

3. Industrial VOC Exhaust Recovery & Thermal Oxidation

Chemical processing and coating facilities produce complex VOC streams containing aromatics, esters, and ketones. Today’s state-of-the-art purification setups utilize Regenerative Catalytic Oxidizers (RCO), Regenerative Thermal Oxidizers (RTO), and active carbon/zeolite concentration wheels to achieve >99% recovery and abatement efficiency.

4. High-Temperature Bio-Hazard & Medical Waste Steam Sterilization

Beyond gaseous purification, industrial biosecurity mandates continuous high-temperature steam treatment for hospital waste and animal residue hydrolysis. Automated vacuum steam autoclaves operating at 134°C–160°C ensure complete pathogen eradication and ecological safety.

Engineering Performance Benchmarks: Conventional Field-Built vs. China 4.0 Skid-Mounted Systems

Performance Metrics Legacy Field-Erected Purification Plants China 4.0 Skid-Mounted Modular Systems Samara Operational Advantage
On-Site Civil & Installation Time 8 - 14 Months 15 - 30 Days Bypasses winter weather construction freezes
Quality Control & Testing Variable field welds & inspections 100% NDT Factory X-Ray & Hydraulic Pressure Tested Zero leakage guarantee under sub-zero thermal cycling
H₂S Removal Efficiency 95.0% - 98.0% > 99.9% (< 4ppm residual H₂S) Fully compliant with pipeline transport standards
Moisture Dew Point -40°C to -50°C Down to -70°C (Molecular Sieve TSA) Prevents freeze-ups in cryogenic liquefaction units
Total Cost of Ownership (TCO) High CAPEX & unexpected field labor overrun 35% - 50% TCO Reduction Optimized capital expenditure with full lifecycle reliability

China 4.0 Supply Chain Integration: Engineered by World-Class Scientists

Combining research from Tsinghua University and the Chinese Academy of Sciences with state-of-the-art skid fabrication capabilities.

78M RMB
Registered Capital Base
A2 Class
Pressure Vessel License
50+
Skid Liquefaction Projects Delivered
20+
Core R&D Technology Patents

Led by World-Renowned Cryogenic & Environmental Process Experts

Dr. Sun Zhaohu
Founder & Chairman | Ph.D., Chinese Academy of Sciences

National Senior Engineer. Headed National 863 Program projects, Natural Science Foundation major funds, and aerospace cryogenic systems. Recipient of Beijing Science and Technology Award (First Prize) and Chinese Society of Refrigeration Special Invention Award.

Dr. Zou Xin
General Manager | Senior Engineer, CAS IPCT

Spearheaded National 12th Five-Year Plan major science initiatives. Published 24 peer-reviewed international academic papers (11 SCI/EI indexed) with 9 authorized national invention patents for gas purification skids.

Dr. Cheng Kuwei
Chief Engineer | Doctor of Engineering, CAS

Pioneer in phase change heat transfer characteristics of mixed refrigerants. Masterminded the process design for skid-mounted natural gas liquefaction systems installed across tough geographic zones.

Manufacturing Facility Certification & Quality Rigor

Operating out of the Sanhe Economic Development Zone industrial cluster in Langfang, Hebei Hongke Qingneng Environmental Protection Equipment Co., Ltd. maintains top-tier international certifications including A2 Class Pressure Vessel Manufacturing License, Pressure Pipeline Component License, GB/T19001-2016 / ISO9001 Quality System Certification, and Sinopec HSSE / China Petroleum HSE Management System Certifications. Every custom pressure vessel, heat exchanger, and skid assembly undergoes rigorous non-destructive testing (NDT), hydrostatic stress verification, and automated process calibration prior to shipment.

Request Technical Dossier & Factory Certification

Localized Purification Equipment Deployments in Samara

Targeted engineering configurations designed to solve specific operational challenges across Volga industrial sectors.

Scenario A: Associated Petroleum Gas (APG) Sweetening in Samara Oilfields

Remote oil production sites in the Volga-Ural basin frequently flare sour associated gas due to high H₂S and heavy hydrocarbon content. Our mobile skid-mounted purification platforms integrate desulphurisation, TSA dehydration, and heavy oil removal into a single compact footprint. This enables direct pipeline injection or on-site LNG liquefaction, converting environmental penalties into liquid energy assets.

Scenario B: Volatile Organic Compound (VOC) Recovery in Petrochemical Plants

Samara’s high-density synthetic rubber, paint coating, and organic synthesis plants release exhaust streams loaded with solvent vapors. By deploying custom VOC Exhaust Treatment Systems (incorporating multi-stage condensation cold traps operating down to -135°C alongside carbon adsorption beds), facilities achieve 99.2% VOC recovery while satisfying strict regional clean-air mandates.

Scenario C: Centralized High-Temperature Medical Waste Sterilization

For municipal healthcare infrastructure and bio-research centers in Samara and Tolyatti, centralized medical waste treatment systems utilize pressurized saturated steam (134°C+) to render surgical waste, laboratory tissue, and sharps completely sterile, safe for clean landfill disposal without hazardous incineration fumes.

Scenario D: Laboratory & Veterinary Carcass Hydrolysis Facilities

High-temperature alkaline hydrolysis treatment equipment designed for biological research labs and agricultural processing. Provides environmentally sound, harmless destruction of animal carcasses and toxic bio-sludge through sealed chemical-thermal reaction chambers.

Engineering Performance & Project Execution Cases

Representative global and domestic skid-mounted equipment deployments across gas purification, waste handling, and cryogenic fields.
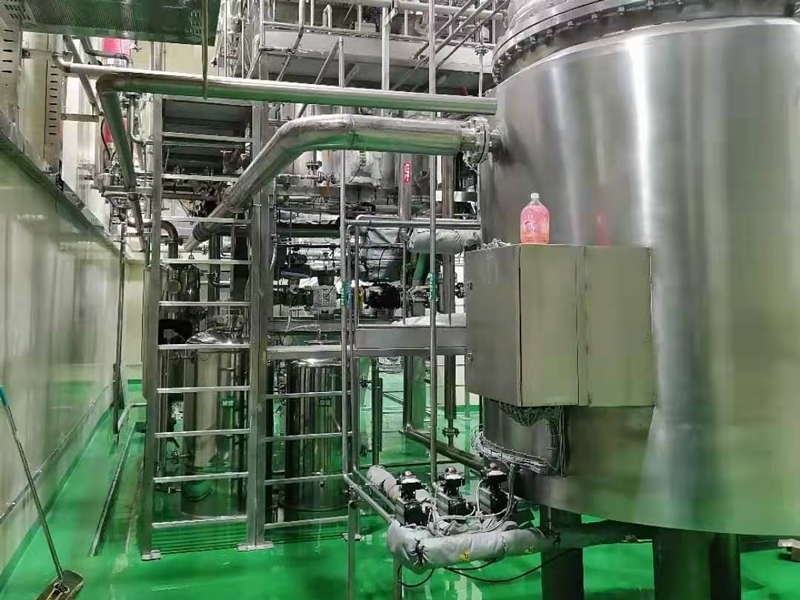
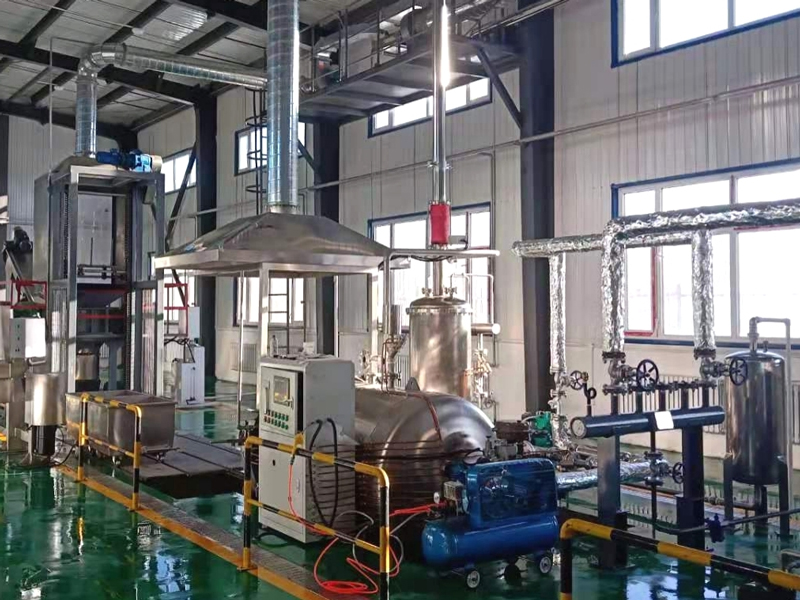
Laboratory Animal Residue Treatment Project
Laboratory Animal Residue Harmless Treatment Project
Mobile Medical Waste Disposal Equipment
Mobile Medical Waste Disposal Equipment System
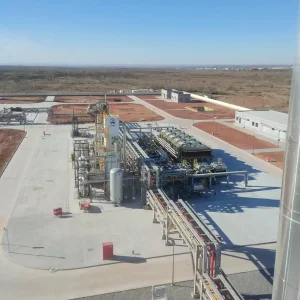
Well Gas Liquefaction Project
Well Gas Purification & Liquefaction Skid Unit
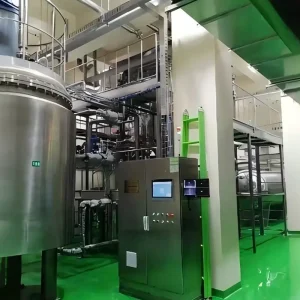
Centralized Medical Waste High Temperature Steam Unit
Centralized Medical Waste High-Temperature Steam System
A2 Pressure Vessel Fabrication
Skid Mount Assembly Workshop
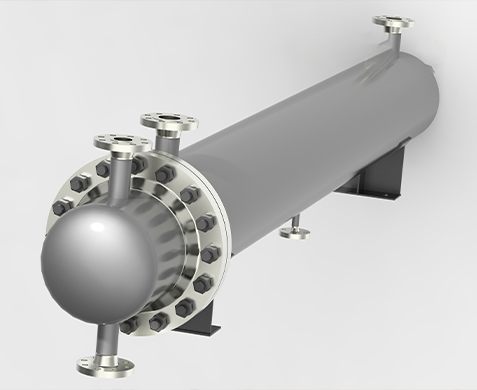
Heat Exchanger Manufacturing
Cryogenic Unit Testing Facility

Planning a Gas Purification or Environmental Retrofit in Samara?

Consult directly with our doctoral R&D engineering team. We supply tailored skid designs, A2 pressure vessel calculations, and rapid turnkey production schedules.

Send Inquiry Now

Frequently Asked Questions by Industrial Procurement Teams

Direct technical answers regarding purification equipment deployment, custom pressure vessels, and Samara regional compliance.

Q1: How do your purification skids handle severe cold winter conditions in the Samara region?
All our outdoor-rated skid platforms engineered for Northern and CIS regions incorporate low-temperature certified steel alloys (such as 09G2S equivalent or 316L stainless steel), electric heat tracing, high-density mineral wool insulation cladding, and fully enclosed containerized shelters. Controls and instrument air systems are heat-jacketed to ensure flawless startup and continuous operation down to -40°C.
Q2: What certifications are provided for custom pressure vessels and desulphurisation columns?
Our manufacturing plant holds the A2 Class Pressure Vessel Manufacturing License, Pressure Pipeline Component License, ISO9001 (GB/T19001-2016) Quality Management Certification, and Petrochemical HSE/HSSE system certifications. We provide complete manufacturing documentation packages, including Material Test Reports (MTRs), 100% Radiographic/Ultrasonic NDT inspection records, hydrostatic pressure test certificates, and third-party inspection compliance.
Q3: Can skid-mounted natural gas purification units handle fluctuating feed gas compositions?
Yes. Our engineering leadership from the Chinese Academy of Sciences has optimized dynamic process simulation models. Our deacidification (amine sweetening) and TSA molecular sieve dehydration skids feature automatic PLC/DCS control loops that dynamically adjust solvent circulation rates and regeneration heater cycles based on real-time gas chromatography feed input.
Q4: What is the typical lead time from contract signing to factory delivery for skid units?
Thanks to our China 4.0 standardized module fabrication workflow in the Sanhe Economic Development Zone, standard skid-mounted purification and VOC recovery packages are delivered within 90 to 120 days—significantly faster than European or local field-erected alternatives.
Q5: What VOC abatement efficiency can your catalytic and thermal exhaust treatment systems guarantee?
Our custom VOC treatment systems (combining zeolite concentration wheels, industrial cold traps down to -135°C, and RCO/RTO oxidizers) achieve continuous destruction and removal efficiencies (DRE) exceeding 99.0%, fully meeting international environmental discharge guidelines.
Q6: How is medical waste and animal carcass hydrolysis equipment certified safe for infectious control?
Our medical waste high-temperature steam sterilization systems operate under multi-stage pulsed vacuum cycles reaching temperatures of 134°C or higher with holding times guaranteed to achieve Log-6 (99.9999%) microbial inactivation. All vessels are manufactured to high-pressure thermal vessel standards with automated safety interlocks.

Comprehensive Industrial Purification & Thermal Processing Equipment

Explore our full lineup of custom pressure vessels, natural gas treatment systems, VOC abatement modules, and biosecurity waste solutions.
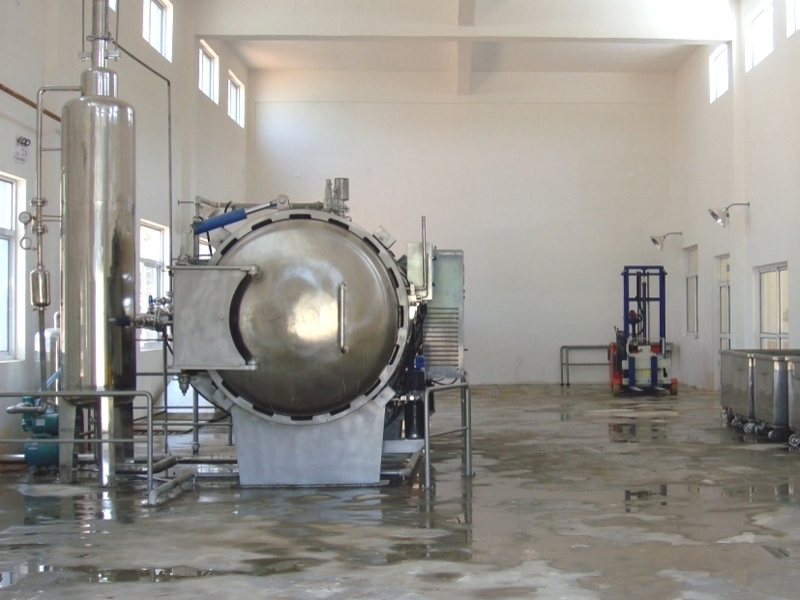
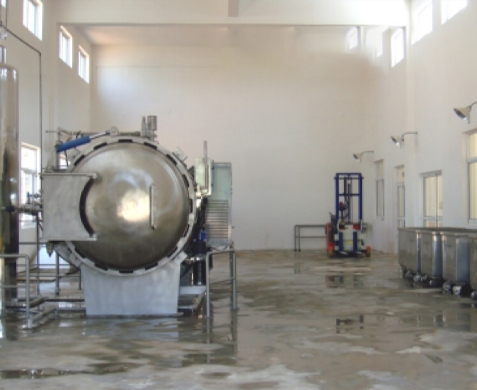
Medical Waste High-Temperature Steam Treatment Equipment

High-Quality Centralized Medical Waste High-Temperature Steam Treatment Equipment from China Suppliers & Factory

Explore Specifications
China VOC Exhaust Treatment Equipment

China VOC Exhaust Treatment Equipment - China Suppliers & Factory for Effective Organic Waste Gas Recovery and Pollution Control Manufacturer, Factories

Explore Specifications
Pet Hydration Chamber

China Suppliers Factory for Environmentally Sound Pet Hydration Chamber for Harmless Pet Treatment

Explore Specifications
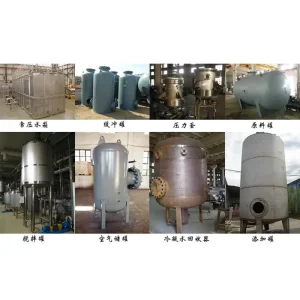
Custom Pressure Vessel Solutions

China Custom Non-Standard Pressure Vessel Solutions from China Suppliers and Factory for Energy and Biopharmaceutical Industries Manufacturers, Manufacturer

Explore Specifications
Centralized Medical Waste High-Temperature Steam Treatment Equipment

China Centralized Medical Waste High-Temperature Steam Treatment Equipment Manufacturer, Factory

Explore Specifications
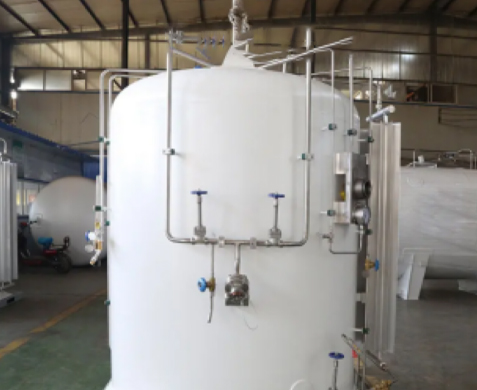
China Liquefaction Plant Solutions

China Liquefaction Plant Life Cycle Solutions by Trusted Suppliers for Efficient Factory Operations

Explore Specifications
High-Temperature Hydrolysis Treatment Equipment for Animal Carcasses

China High-Temperature Hydrolysis Treatment Equipment for Laboratory Animal Carcasses - China Suppliers & Factory Supplier, Factory

Explore Specifications
Laboratory Animal Carcasses Hydrolysis Equipment

High-Quality High-Temperature Hydrolysis Treatment Equipment for Laboratory Animal Carcasses from China Suppliers and Factory Supplier, Factories

Explore Specifications

Natural Gas & VOC Exhaust Treatment Platforms

Natural Gas Treatment Plant Exhaust Gas Recovery Equipment

China Suppliers Factory for Natural Gas Treatment Plant Exhaust Gas Recovery Equipment

Explore Specifications
Advanced Desulphurisation Equipment

China Suppliers and Factory for Advanced Desulphurisation Equipment in Natural Gas Processing

Explore Specifications
VOC Exhaust Treatment Equipment Manufacturers

China VOC Exhaust Treatment Equipment Manufacturers, Factory

Explore Specifications
Natural Gas Exhaust Gas Recovery Equipment

China Natural Gas Treatment Plant Exhaust Gas Recovery Equipment - Suppliers & Factory Solutions for Green Production

Explore Specifications

Partner with China’s Leading Purification Equipment Manufacturer

Whether you require custom pressure vessels, skid-mounted H₂S desulphurisation plants, VOC treatment systems, or cryogenic LNG units tailored for Samara and global installations, our engineering team delivers unparalleled precision and cost-efficiency.

Send Inquiry Now